EN

Translate:

HuaBang
  • Home
  • Profile
  • Qualification
  • PRODUCT
    • Flaking Cooling Systems
    • Granulation System
    • Packaging System
    • Conveying System
    • VOC Treatmemt
    • Reactor
    • Axial Flow Pump
    • Screening Classification
    • Baghouse Dust Collectors
    • EPC Basis
  • Update
  • BLOG
  • More
    • Home
    • Profile
    • Qualification
    • PRODUCT
      • Flaking Cooling Systems
      • Granulation System
      • Packaging System
      • Conveying System
      • VOC Treatmemt
      • Reactor
      • Axial Flow Pump
      • Screening Classification
      • Baghouse Dust Collectors
      • EPC Basis
    • Update
    • BLOG
HuaBang

EN

  • Home
  • Profile
  • Qualification
  • PRODUCT
    • Flaking Cooling Systems
    • Granulation System
    • Packaging System
    • Conveying System
    • VOC Treatmemt
    • Reactor
    • Axial Flow Pump
    • Screening Classification
    • Baghouse Dust Collectors
    • EPC Basis
  • Update
  • BLOG

Conveying Systems

Section Overview

Tianjin Huabang supplies conveying systems as part of an integrated downstream solids-handling platform for flakes, granules, and moderately free-flowing powders. These systems are engineered to connect flaking, screening, storage, and packaging in a stable, low-loss, and plant-friendly manner. The conveying portfolio is intended for cont

Tianjin Huabang supplies conveying systems as part of an integrated downstream solids-handling platform for flakes, granules, and moderately free-flowing powders. These systems are engineered to connect flaking, screening, storage, and packaging in a stable, low-loss, and plant-friendly manner. The conveying portfolio is intended for continuous industrial duty in chemical and related process industries, with emphasis on controlled transfer, enclosed operation, equipment compatibility, and straightforward integration into automated production lines.

In practical project execution, conveying equipment is not selected as an isolated utility. It is selected as a process link that must match the material form, conveying distance, required elevation, dust-control philosophy, plant layout, and downstream feeding precision. For this reason, Huabang organizes its conveying solutions into several complementary equipment families rather than promoting a single universal design.

The core conveying portfolio includes

Screw Conveyors and Screw Feeders

Screw Conveyors and Screw Feeders

Screw Conveyors and Screw Feeders

For horizontal, inclined, or short vertical transfer of flakes, granules, and moderately free-flowing solids, with good enclosure and strong adaptability to process interfaces

Bucket Elevators

Screw Conveyors and Screw Feeders

Screw Conveyors and Screw Feeders

For efficient vertical lifting in limited floor space and for stable transfer to higher storage or packaging points

Belt Conveyors and Belt Feeders

Screw Conveyors and Screw Feeders

Belt Conveyors and Belt Feeders

For gentle transfer over medium distances, especially where product degradation must be minimized, and stable continuous flow is important

Vibratory Conveyors

Pneumatic Conveying Systems

Belt Conveyors and Belt Feeders

For controlled transfer, spreading, and gentle movement of solids, particularly useful where low material breakage and clean discharge are important

Pneumatic Conveying Systems

Pneumatic Conveying Systems

Pneumatic Conveying Systems

For enclosed transfer of granules and selected powders over longer distances, especially where dust control, routing flexibility, or plant cleanliness is a priority

Product Positioning and Engineering Approach

Huabang conveying systems are designed for industrial production environments in which reliability, containment, and maintainability are as important as nominal throughput. The engineering focus is not only on moving the product, but on preserving product quality and ensuring stable operation of the full line

This is particularly important in downstream systems handling:

  • laked products that must not be excessively broken
  • granules that must remain free-flowing
  • materials that may produce nuisance dust
  • heated or recently solidified products that require controlled handling
  • chemical products that demand corrosion resistance or enclosed transfer

Conveying-system design is developed around five practical e

Material Form

Layout and Distance

Material Form

Flakes, granules, and moderately free-flowing powders do not behave in the same way. Product geometry determines the most suitable conveying principle, the internal clearances, transfer points, and anti-bridging measures

Process Duty

Layout and Distance

Material Form

Conveying may serve simple transfer, controlled feeding, elevation, buffering, or line balancing. The selected machine must therefore match not only capacity, but also the role it plays in the process

Layout and Distance

Layout and Distance

Containment Requirement

Short transfer between connected equipment may favor screw or vibratory designs, while longer or more complex routing may justify belt or pneumatic systems

Containment Requirement

Containment Requirement

Containment Requirement

Where dust control, odor control, or enclosed operation is required, the conveyor must support sealed interfaces and easy integration with local exhaust or dust-collection systems

Downstream Stability

Containment Requirement

Downstream Stability

Packaging lines, screening systems, and storage hoppers all depend on consistent feed. Conveyors must therefore deliver stable, non-pulsing product flow within the required capacity window

Key Technical Features

Compact and Enclosed Construction

Compact and Enclosed Construction

Compact and Enclosed Construction

Screw conveyors provide a compact mechanical layout and are well-suited to installation beneath flakers, bins, and hoppers. The enclosed casing helps reduce product loss, dust escape, and environmental contamination

Strong Process Integration

Compact and Enclosed Construction

Compact and Enclosed Construction

Because the inlet and outlet arrangement can be adapted easily, screw conveyors are effective as direct interconnecting equipment between upstream and downstream machines. This makes them particularly useful in packaged skid systems and compact plant layouts

Flexible Feeding Characteristics

Compact and Enclosed Construction

Flexible Feeding Characteristics

Short transfer between connected equipment may favor screw or vibratory designs, while longer or more complex routing may justify belt or pneumatic systems

Containment Requirement

Containment Requirement

Flexible Feeding Characteristics

Where dust control, odor control, or enclosed operation is required, the conveyor must support sealed interfaces and easy integration with local exhaust or dust-collection systems

Downstream Stability

Containment Requirement

Downstream Stability

Packaging lines, screening systems, and storage hoppers all depend on consistent feed. Conveyors must therefore deliver stable, non-pulsing product flow within the required capacity window

Screw Conveyor Selection Table

Common design basis for the series

Execution: tubular or U-trough screw conveyor
Installation: horizontal or inclined
Drive: geared motor with variable-frequency option
Construction: carbon steel, SS304 or SS316L according to service requirement

Actual capacity depends on bulk density, product flowability, inclination, moisture level, inlet condition, and required fill factor

Customization Options

Available options include:

  • shafted or shaftless screw arrangement
  • variable pitch or special flight design
  • quick-open covers for cleaning and inspection
  • anti-bridging feed hopper
  • wear-resistant liners
  • gas-tight or dust-tight sealing arrangement
  • feed-control instrumentation and interlocks
  • explosion-proof motor and instrument package
Screw Conveyor Selection Table

Common design basis for the series

Execution: tubular or U-trough screw conveyor
Installation: horizontal or inclined
Drive: geared motor with variable-frequency option
Construction: carbon steel, SS304 or SS316L according to service requirement

Actual capacity depends on bulk density, product flowability, inclination, moisture level, inlet condition, and required fill factor

Customization Options

Available options include:

  • shafted or shaftless screw arrangement
  • variable pitch or special flight design
  • quick-open covers for cleaning and inspection
  • anti-bridging feed hopper
  • wear-resistant liners
  • gas-tight or dust-tight sealing arrangement
  • feed-control instrumentation and interlocks
  • explosion-proof motor and instrument package

Bucket Elevators

Product Description

Bucket elevators are used where material must be lifted vertically with high efficiency and minimal floor space. They are especially suitable for transferring flakes or granules from lower process elevations to storage bins, buffer hoppers, or packaging floors.

Material is loaded into a series of buckets attached to a belt or chain. The bu

Bucket elevators are used where material must be lifted vertically with high efficiency and minimal floor space. They are especially suitable for transferring flakes or granules from lower process elevations to storage bins, buffer hoppers, or packaging floors.

Material is loaded into a series of buckets attached to a belt or chain. The buckets travel upward within an enclosed casing and discharge the material at the top through centrifugal or gravity-type unloading, depending on product behavior and system design.

Typical Applications

Bucket elevators are commonly used for:

  • lifting flaked product to storage silos or day bins
  • feeding elevated screening or packaging stations
  • vertical transfer in multi-floor process buildings
  • space-efficient integration into compact production layouts

Key Technical Features

Efficient Vertical Transfer

Good Capacity-to-Footprint Ratio

Good Capacity-to-Footprint Ratio

Bucket elevators provide a large vertical lift within a small footprint, making them well-suited to plants where horizontal space is limited

Good Capacity-to-Footprint Ratio

Good Capacity-to-Footprint Ratio

Good Capacity-to-Footprint Ratio

Compared with inclined conveyors that occupy large floor space, the bucket elevator offers a cleaner, more compact route for product elevation

Enclosed Product Path

Configurable Bucket and Discharge Design

Configurable Bucket and Discharge Design

The closed casing supports cleaner handling and reduced material loss. It also makes integration with dust control easier in areas where product fines may be present

Configurable Bucket and Discharge Design

Configurable Bucket and Discharge Design

Configurable Bucket and Discharge Design

Bucket shape, spacing, and discharge arrangement can be selected to suit flakes, granules, or other bulk solids, reducing material hang-up and improving discharge stability

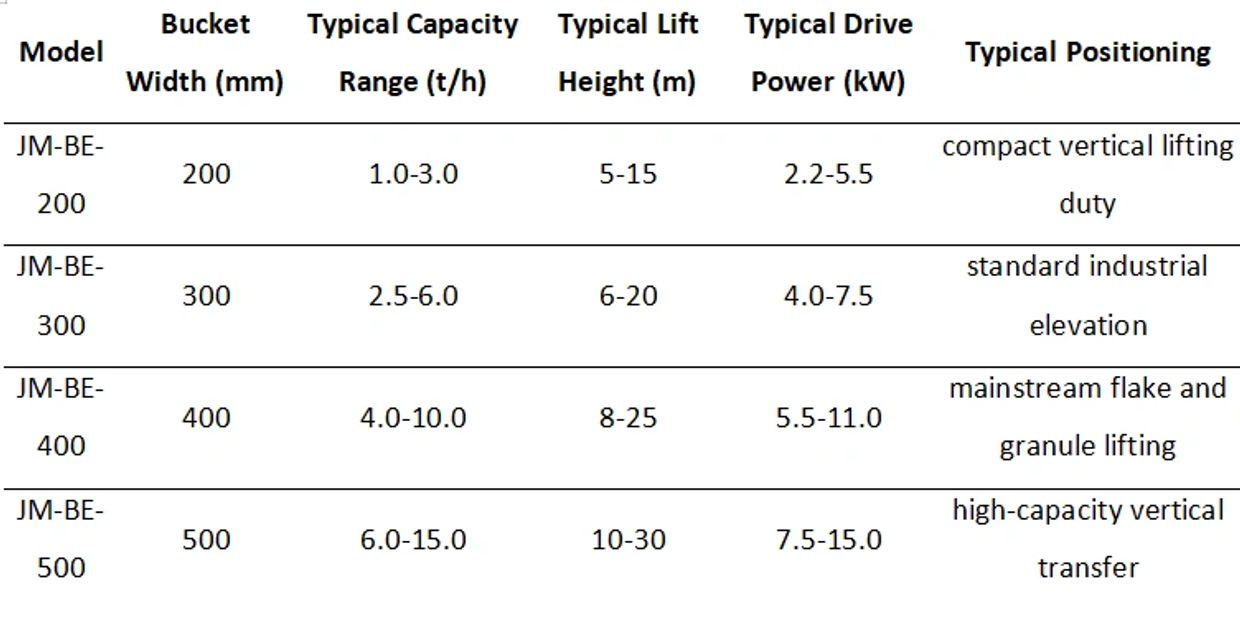
Bucket Elevator Selection Table

Common design basis for the series

Execution: belt or chain type
Construction: carbon steel, SS304 or SS316L
Arrangement: vertical lift with enclosed casing

Actual performance depends on product bulk density, bucket fill efficiency, lift height, and discharge behavior

Customization Options

Available options include:

  • belt-type or chain-type arrangement
  • anti-backstop device
  • explosion relief and venting interface
  • inspection doors and maintenance platforms
  • wear-resistant boot section
  • level switch and blockage alarm
  • integrated inlet hopper and discharge chute design
Belt Conveyors and Belt Feeders

Product Description

Belt conveyors are selected for gentle, stable transfer over medium distances. They are especially suitable for flakes and granules that should be handled with minimal breakage or compression.

In a belt conveyor, the product travels on a continuously moving belt supported by rollers or a slider bed. Because the product rests on the belt ra

Belt conveyors are selected for gentle, stable transfer over medium distances. They are especially suitable for flakes and granules that should be handled with minimal breakage or compression.

In a belt conveyor, the product travels on a continuously moving belt supported by rollers or a slider bed. Because the product rests on the belt rather than being mechanically pushed or agitated, this conveying principle is well-suited to applications where product preservation and clean discharge are important.

Typical Applications

Belt conveyors are commonly used for:

  • transfer of flaked product to screening or packaging
  • gentle movement of the finished product to storage
  • horizontal or mildly inclined transport between process areas
  • discharge from the breaker, screener, or inspection station

Key Technical Features

Gentle Product Handling

Gentle Product Handling

Gentle Product Handling

The belt conveyor is often preferred where flake integrity must be preserved and product attrition minimized

Stable Continuous Flow

Gentle Product Handling

Gentle Product Handling

The belt provides a smooth conveying profile with minimal pulsation, which is beneficial when downstream equipment requires a steady and predictable product load

Flexible Layout

Adaptable as Conveyor or Feeder

Adaptable as Conveyor or Feeder

The machine can be configured with different lengths, inclinations, and discharge arrangements to suit the plant layout

Adaptable as Conveyor or Feeder

Adaptable as Conveyor or Feeder

Adaptable as Conveyor or Feeder

With proper weighing or speed control, the same platform can be used not only for transport but also for controlled feeding to downstream equipment

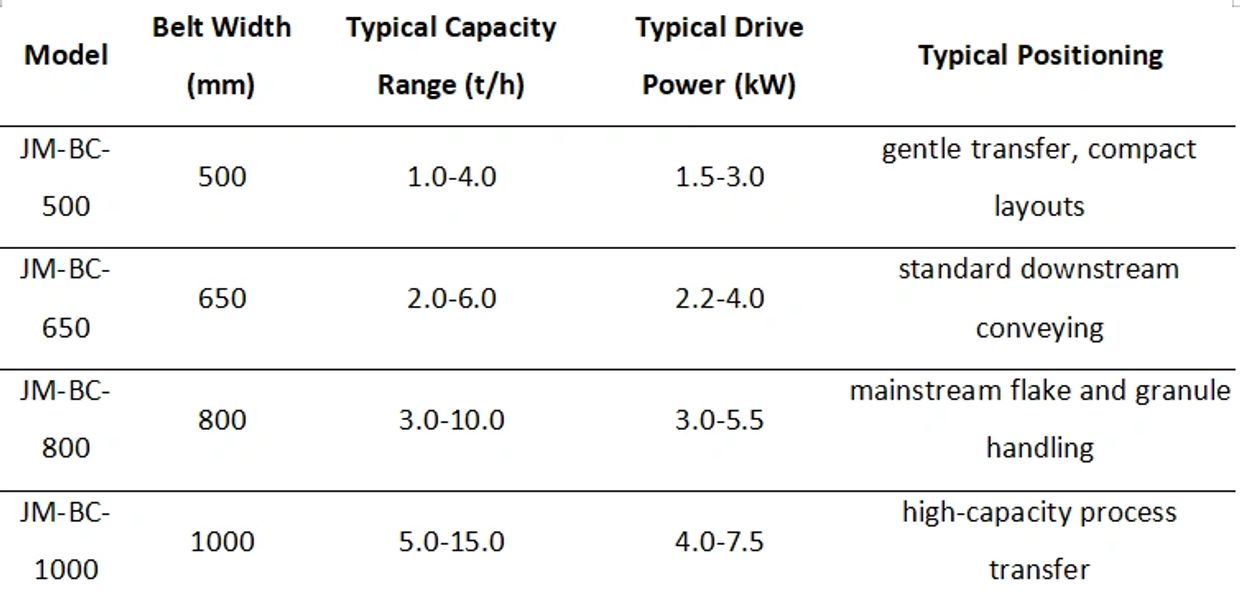
Belt Conveyor Selection Table

Common design basis for the series

Belt width: selected according to capacity and product bed depth
Construction: carbon steel or stainless steel frame
Belt type: smooth, cleated or food/chemical-grade according to service

Actual capacity depends on material bulk density, belt speed, belt inclination, and allowable bed depth

Customization Options

Available options include:

  • smooth or cleated belt
  • enclosed covers and side sealing
  • belt weighing arrangement
  • receiving hopper and discharge chute
  • support legs, platforms, and walkways
  • integrated metal detector or checkweigher interface
  • reversible or fixed-direction operation

Vibratory Conveyors

Product Description

Vibratory conveyors provide controlled movement of solids through vibration rather than continuous dragging or pushing by a mechanical element. They are especially suitable for applications where gentle handling, controlled spread, and clean discharge are required.

The conveyor tray is excited by a vibratory drive, causing the product to a

Vibratory conveyors provide controlled movement of solids through vibration rather than continuous dragging or pushing by a mechanical element. They are especially suitable for applications where gentle handling, controlled spread, and clean discharge are required.

The conveyor tray is excited by a vibratory drive, causing the product to advance in small repeated movements. Because the product is moved in a shallow bed with limited mechanical compression, this method can be beneficial for fragile flakes or for controlled product distribution ahead of screening or packaging.

Typical Applications

Vibratory conveyors are commonly used for:

  • flake discharge and spreading
  • transfer to screeners or inspection points
  • controlled feeding to packaging or accumulation hoppers
  • low-breakage movement of fragile products

Key Technical Features

Gentle Product Transport

Good for Controlled Distribution

Good for Controlled Distribution

The shallow-bed transport mechanism can reduce product degradation compared with more aggressive conveying methods

Good for Controlled Distribution

Good for Controlled Distribution

Good for Controlled Distribution

Vibratory conveyors are useful when the product needs to be spread evenly before entering another machine

Compact and Clean Design

Simple Mechanical Principle

Simple Mechanical Principle

The equipment can be built in a relatively compact format and is easy to integrate into enclosed or semi-enclosed process arrangements

Simple Mechanical Principle

Simple Mechanical Principle

Simple Mechanical Principle

With fewer moving internal contact components than some other conveyor types, the vibratory conveyor can provide reliable service within its proper duty range

Vibratory Conveyor Selection Table

Actual capacity depends on product size, bed depth, vibration setting, and required conveying length
Pneumatic Conveying Systems

Product Description

Pneumatic conveying systems are used where enclosed transfer over longer distances is required, or where the routing flexibility of pipework offers a strong plant-layout advantage. These systems are generally applied to granules and selected powders rather than fragile flakes, unless the product can tolerate the conveying conditions.

Mater

Pneumatic conveying systems are used where enclosed transfer over longer distances is required, or where the routing flexibility of pipework offers a strong plant-layout advantage. These systems are generally applied to granules and selected powders rather than fragile flakes, unless the product can tolerate the conveying conditions.

Material is introduced into an air stream and conveyed through a pipeline to the receiving point. Depending on product characteristics and process requirements, the system may be designed as a dilute-phase or denser, lower-velocity transfer.

Typical Applications

Pneumatic systems are commonly used for:

  • transfer of granules to storage or packaging zones
  • enclosed movement of selected powders
  • routing through congested or multi-level plant areas
  • dust-controlled transfer where open conveyors are undesirable

Key Technical Features

Highly Enclosed Transfer Path

Highly Enclosed Transfer Path

Highly Enclosed Transfer Path

The pipeline system provides robust containment and helps reduce dust emissions into the plant environment

Flexible Routing

Highly Enclosed Transfer Path

Highly Enclosed Transfer Path

Pipelines can be routed around structural and layout constraints more easily than many mechanical conveyors

Clean Plant Integration

Configurable Receiving and Filtering

Configurable Receiving and Filtering

Pneumatic systems are suitable where material transfer must be combined with tidy plant layout and minimal open handling

Configurable Receiving and Filtering

Configurable Receiving and Filtering

Configurable Receiving and Filtering

The system may include filters, receivers, rotary valves, and air-material separation arrangements, depending on the product and duty

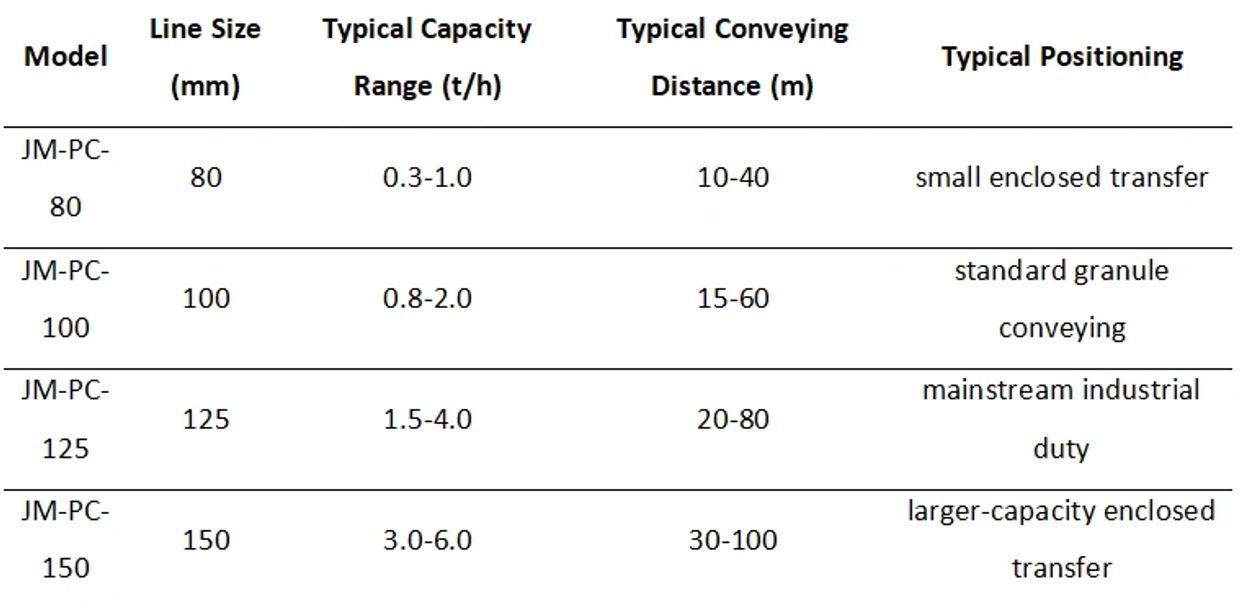
Pneumatic Conveying Selection Table

Common design basis for the series

Execution: pressure or vacuum conveying
Material form: granules and selected powders
Construction: carbon steel or stainless steel pipeline and receiver

Actual performance depends on particle size, density, friability, line routing, conveying pressure, and air-to-solids ratio

Customization Options


Available options include:

  • vacuum or pressure mode
  • receiver and filter module
  • rotary valve or screw feeder inlet
  • anti-abrasion elbows
  • explosion isolation provisions
  • PLC-based pressure and sequence control
  • integration with silo, hopper, and bagging systems

COPYRIGHT © 2000-2026 TIANJIN HUABANG NEW MATERIAL TECHNOLOGY  CO., LTD. -  ALL RIGHTS RESERVED.

  • Home
  • Profile
  • Qualification
  • Flaking Cooling Systems
  • Granulation System
  • Packaging System
  • Conveying System
  • VOC Treatmemt
  • Reactor
  • Axial Flow Pump
  • Screening Classification
  • Baghouse Dust Collectors
  • EPC Basis
  • Update
  • BLOG

Powered by

Cookie Policy

This website uses cookies. By continuing to use this site, you accept our use of cookies.

Accept & Close